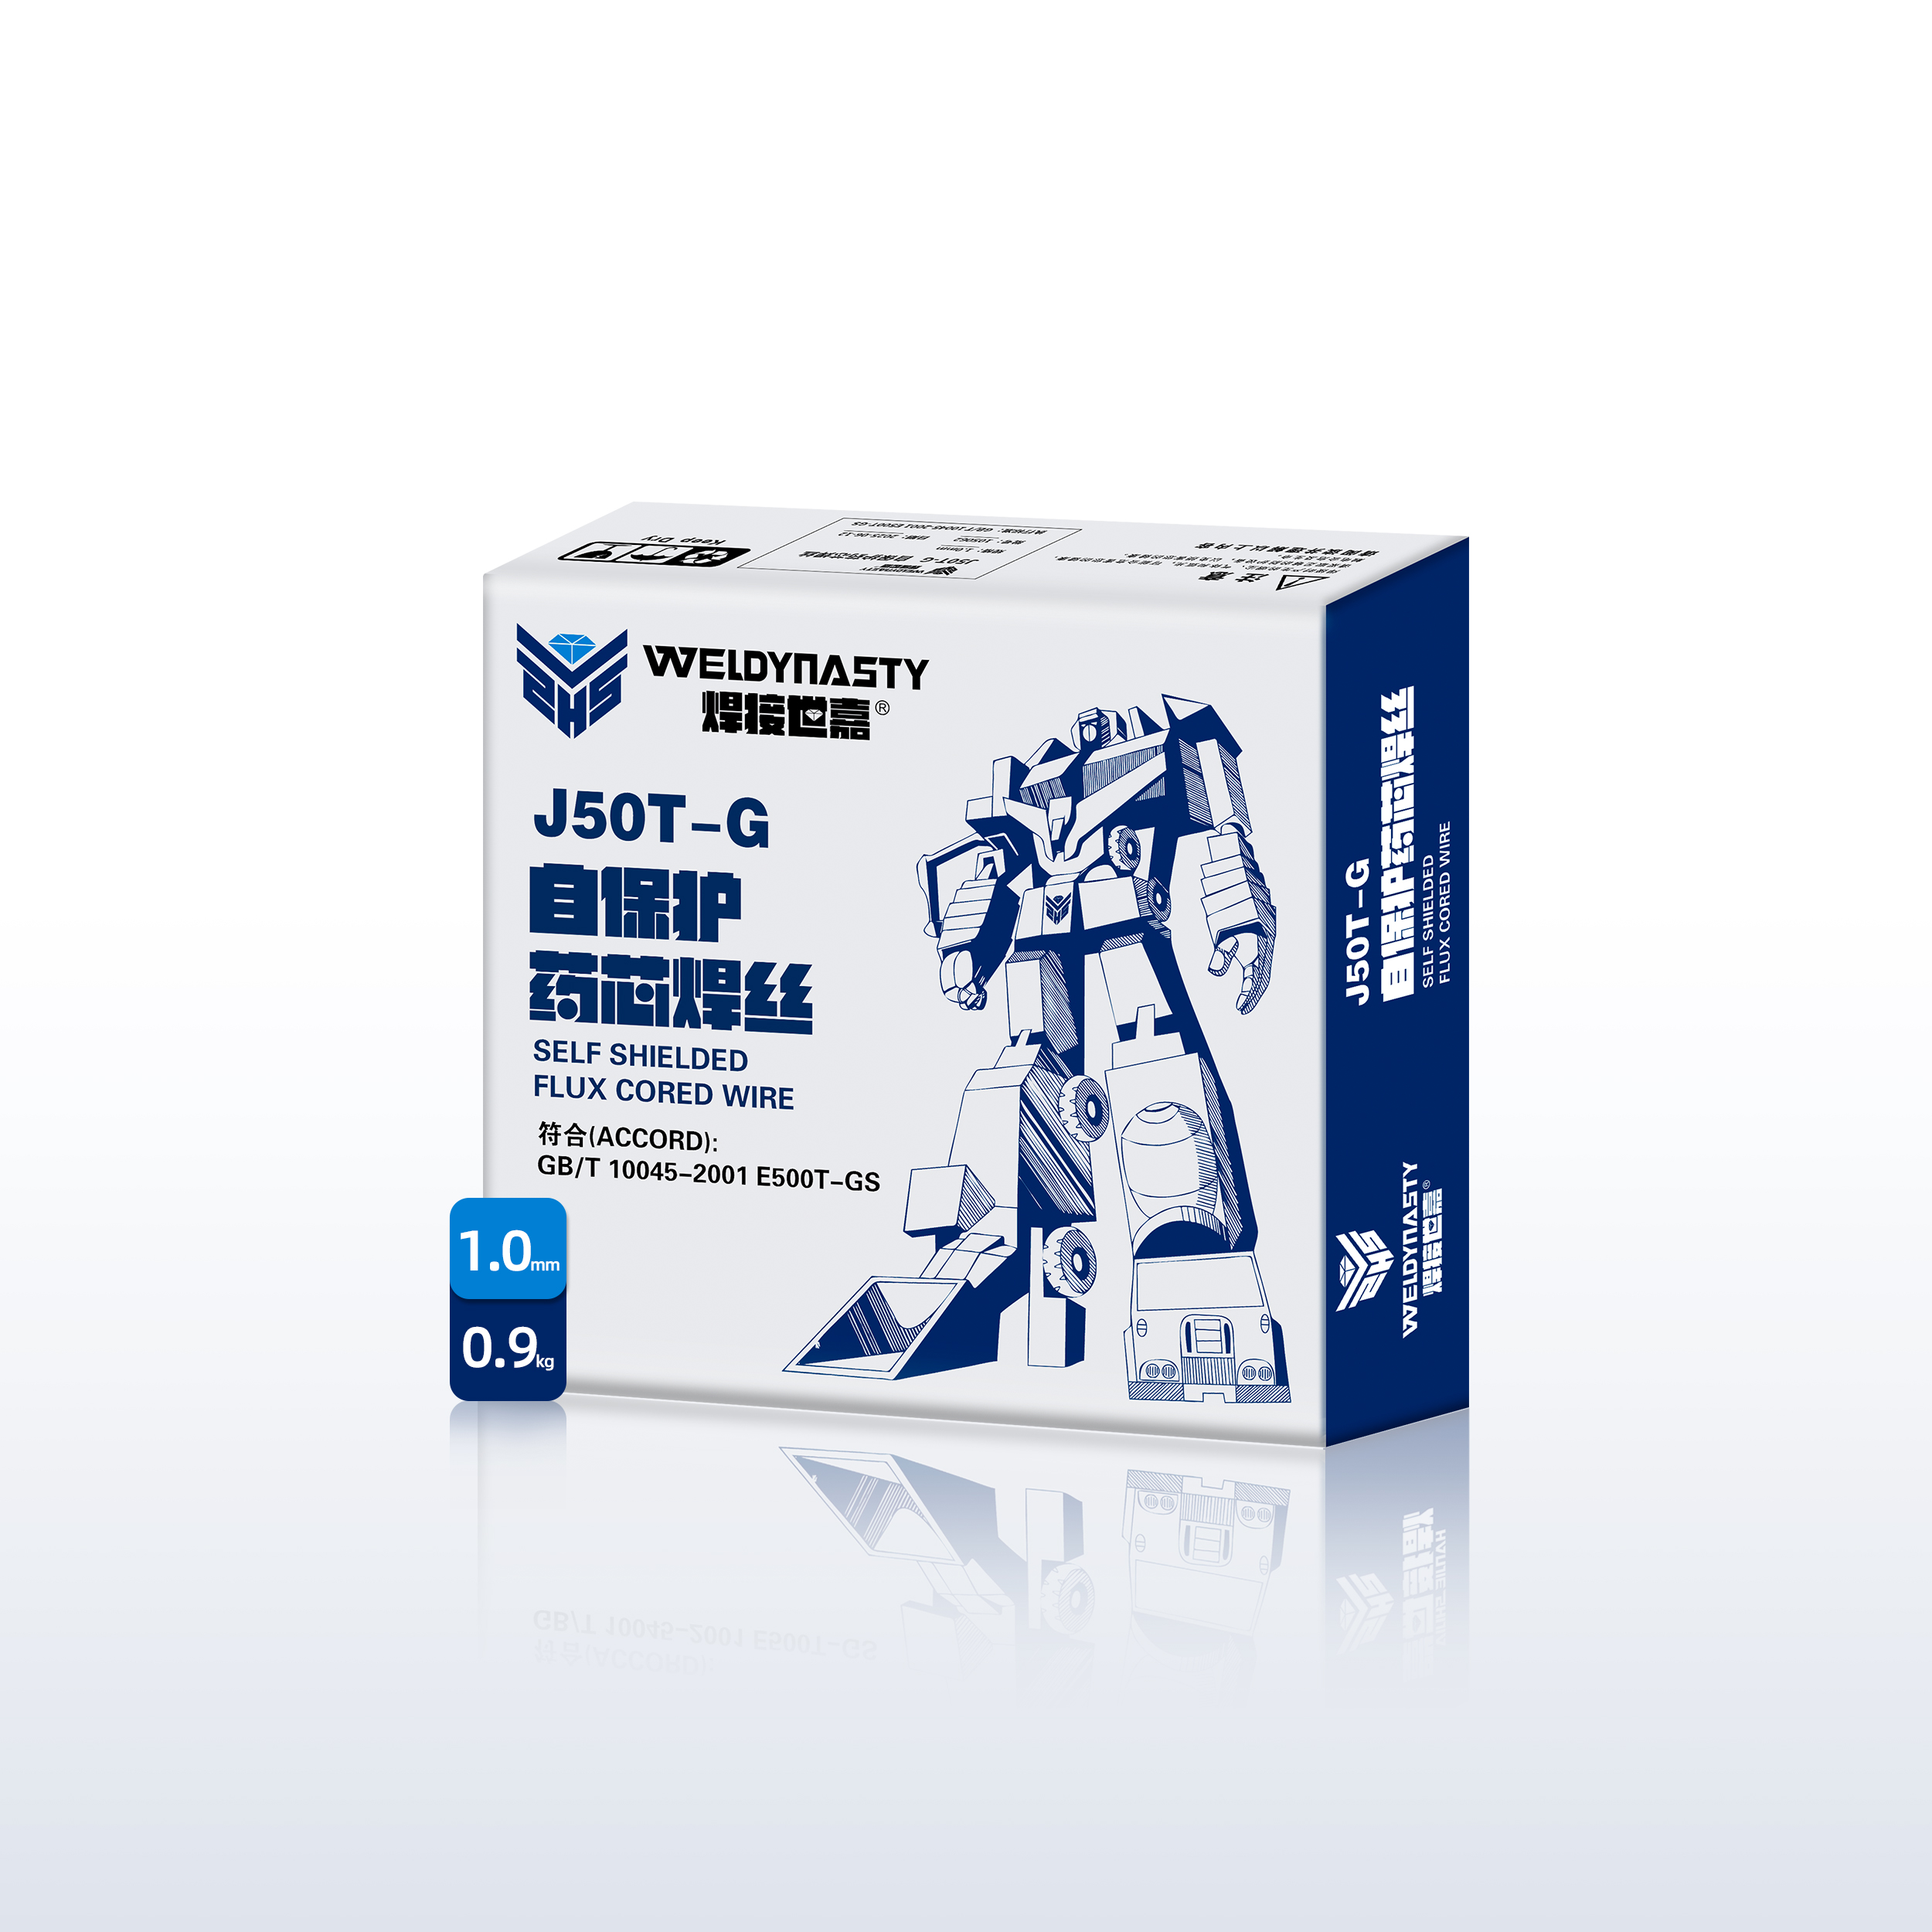

E71T-GS (J50T-G) Self-Shielded Flux-Cored Welding Wire – All-Position, Outdoor, No External Shielding Gas
Designed for outdoor and high-altitude welding, the Weldynasty E71T-GS is a high quality self-shielded flux-cored wire for carbon steel. The flux core contains slag-forming and gas-forming agents that generate gas and slag under arc heat to protect the droplets and weld pool. No external shielding gas is required, which simplifies the torch, reduces weight, and increases welding flexibility. The wire can be used with a household 220 V power supply and offers higher deposition efficiency, lower spatter, better bead appearance, and lower overall cost than conventional manual electrodes.
Key Features:
Self-shielded flux-cored wire offers excellent convenience. 350 A and 500 A gas-shielded welding machines can be used directly after polarity adjustment. The dedicated welding machine is priced only at the level of an ordinary manual electrode welding machine. Compared with ordinary manual electrodes, overall cost is 52% lower and welding efficiency is 61% higher (data from experimental conditions).
Self-Shielded Operation
No external shielding gas source is required; the torch structure is simple, lightweight, and easy to operate. The flux core forms a protective atmosphere through its own metallurgical reaction.
Wind & Porosity Resistance
Good resistance to wind and porosity. It can weld under Grade 4 wind conditions (wind speed ≤ 8 m/s) without additional protection, making it especially suitable for field construction.
Arc Penetration & Droplet Transfer
High arc penetration; spray-like droplet transfer; low spatter.
All-Position & Vertical-Down Performance
Excellent all-position and vertical-down welding process performance; good operability.
Slag Removal
Good slag detachability.
Low-Temperature Toughness in Harsh Conditions
The deposited metal can achieve high low-temperature toughness under low-temperature and strong-wind conditions.
Specifications:
Typical Chemical Composition (%)
| C | Si | Mn | P | S |
| ≤0.18 | ≤0.90 | ≤2.00 | ≤0.03 | ≤0.03 |
Typical Mechanical Property
| Tensile Strength (Rm) MPa | Yield Strength (ReL/Rp0.2) MPa | Elongation (A) % | Impact Toughness (KV₂ at ___°C) J |
| ≥490 | — | — | — |
Classification: AWS A5.36/A5.36M E71T-GS, GB/T 10045-2018 T49TG-1NS
Type: Self-shielded flux-cored wire for carbon steel
Polarity: DC- (DCEN; workpiece positive, welding torch negative)
Shielding Gas:No external shielding gas required
Gas Flow Rate:Not applicable (no external shielding gas)
Available Diameters: Φ0.8, Φ1.0 mm
Welding Positions:Flat, fillet, overhead, vertical-up, vertical-down
Packaging:0.9kg/spool, 4.5 kg/spool (standard); other packaging formats available (per requirement)
Operating Requirements
- Power source: Use a dedicated DC power source or inverter power source.
- Polarity: DCEN (DC-): workpiece positive, welding torch negative. Reversed polarity causes high spatter, shallow penetration, and failure to weld.
- Wire angle for vertical-down welding: Generally 80°–90° to the workpiece. Avoid near-vertical position to prevent slag and molten metal from running down, which can cause slag inclusion and porosity.
- Stick-out: Generally 6–10 times the wire diameter. Excessive stick-out causes the wire to melt too fast and reduces arc force.
- Surface preparation: The surface to be welded should be uniform and smooth, free from rust, slag scale, oil, grease, and other harmful substances.
- Grounding: Keep the welding ground cable as close to the welding zone as possible and confirm good conductivity. Check for oxidation, secure connection, and no rust at the contact point with the base metal. Poor conductivity causes arc instability.
- Parameter adjustment: Directly affects weld quality. Too high current can cause burn-through, increased spatter, downward flow of slag and molten metal in vertical-down welding, and porosity. Too low current can cause incomplete penetration and slag inclusion. Too low voltage can cause arc instability, wire stubbing, difficult pool opening, and slag inclusion. Too high voltage can cause the arc to be too far from the pool, air entrainment, and porosity.
Ideal For
- Welding of outdoor carbon steel, low-alloy steel, and galvanized structural parts, such as advertising frames, street guardrails, doors and windows, nurseries, greenhouse construction and renovation projects.
- Suitable for outdoor and high-altitude operations.