
Flux-Cored vs. Solid – Key Advantages
Compared with solid wire, the 71T-1 Series flux-cored wire offers a significantly higher deposition rate, allowing more weld metal to be deposited per unit of time for greater productivity.The flux core also improves current density, promoting faster wire melting and further boosting deposition efficiency.
Smooth Arc & Clean Welding
The rutile (titania) flux formulation delivers a soft and stable arc, minimal spatter, and easy slag detachability. Weld beads are smooth and well-formed, reducing post-weld cleaning time and improving overall productivity.
All-Position Capability with High Deposition Efficiency
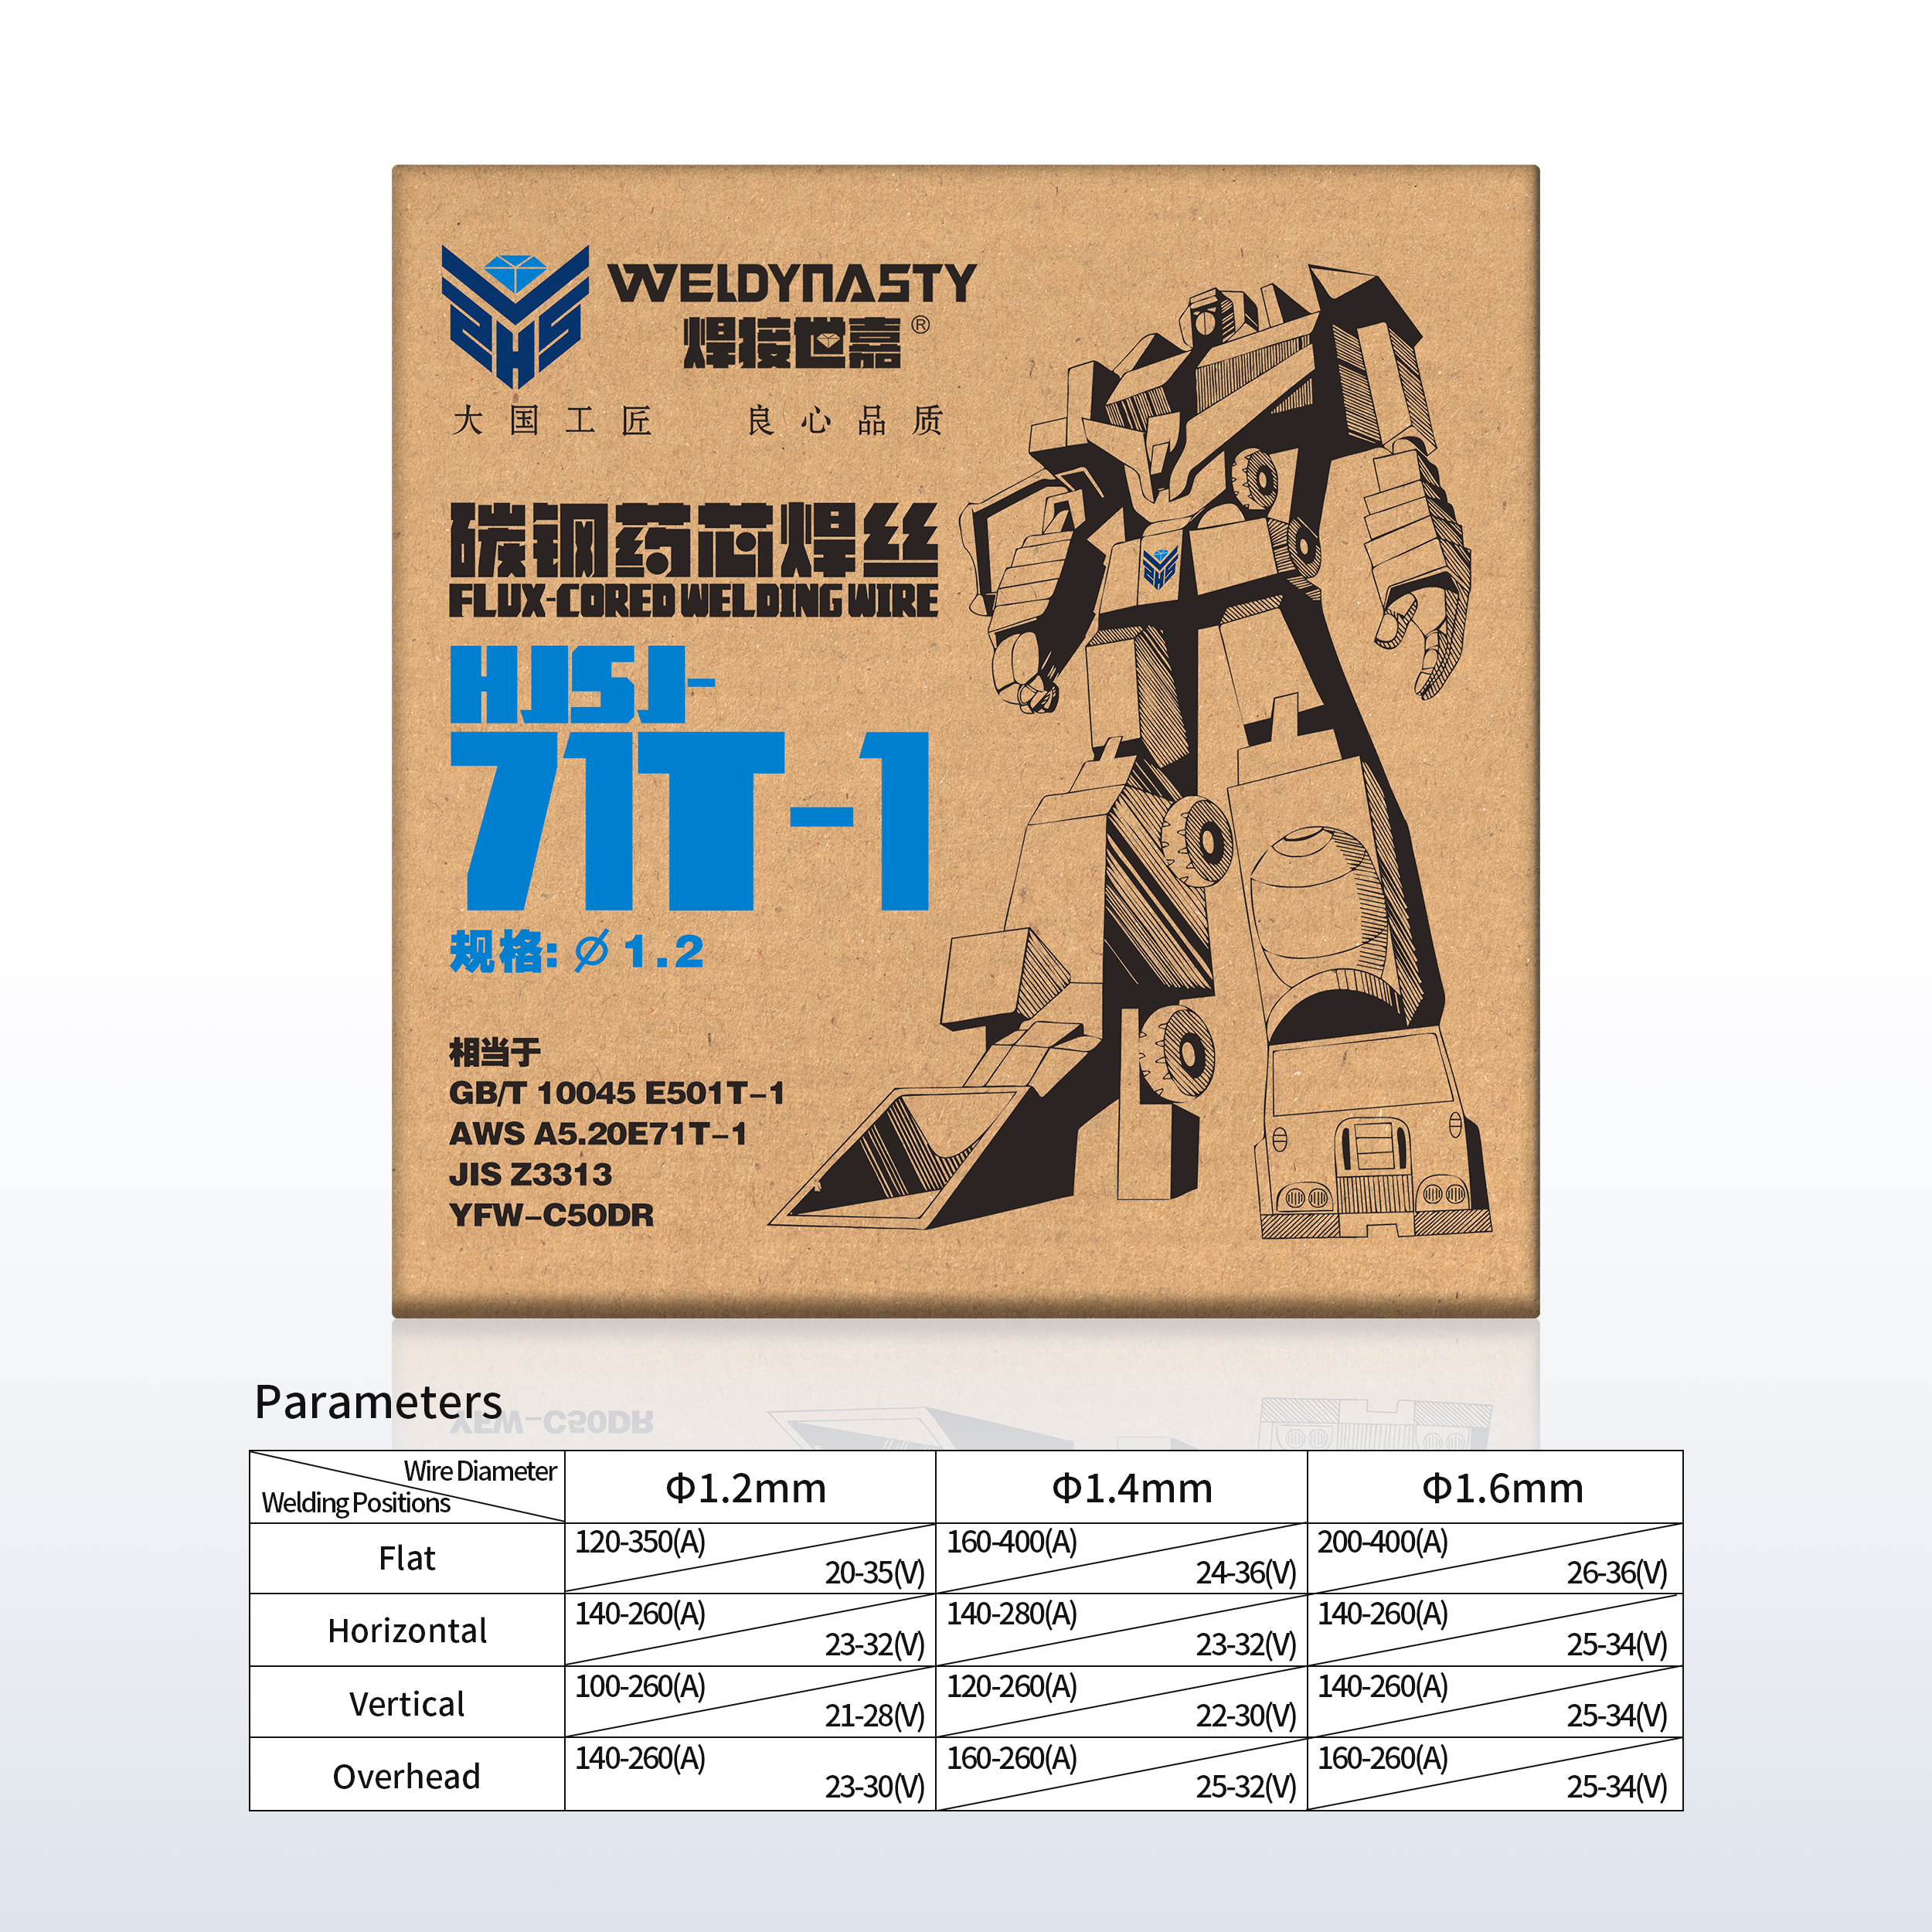
Suitable for flat and horizontal welding, as well as all-position operation, the wire supports efficient, high-deposition welding across diverse joint configurations. This makes it adaptable to both shop fabrication and field work.
Micro-Alloyed Deposit – Low-Temperature Toughness & Crack Resistance
The deposited metal is micro-alloyed for enhanced low-temperature impact toughness and crack resistance. Internal quality is stable and reliable, meeting the demands of critical structural applications.
Stable Performance with CO₂ Shielding
Designed for 100% CO₂ gas shielding, the wire maintains consistent arc characteristics and weld quality when used with gas purity of 99.98% or higher.
Specifications:
| C | Si | Mn | P | S | Ni | Cr | V | Mo |
| ≤0.18 | ≤0.90 | ≤2.00 | ≤0.03 | ≤0.03 | ≤0.05 | ≤0.20 | ≤0.08 | ≤0.30 |
Typical Mechanical Property
| Tensile Strength (Rm) MPa | Yield Strength (ReL/Rp0.2) MPa | Elongation (A) % | Impact Toughness (KV₂ at -20°C) J |
| 490-670 | ≥390 | ≥18 | ≥27 |
Type: CO₂ gas-shielded flux-cored wire
Polarity: DC+ (Direct Current Electrode Positive)
Shielding Gas:100% CO₂, purity ≥ 99.98%
Gas Flow Rate: 20–25 L/min
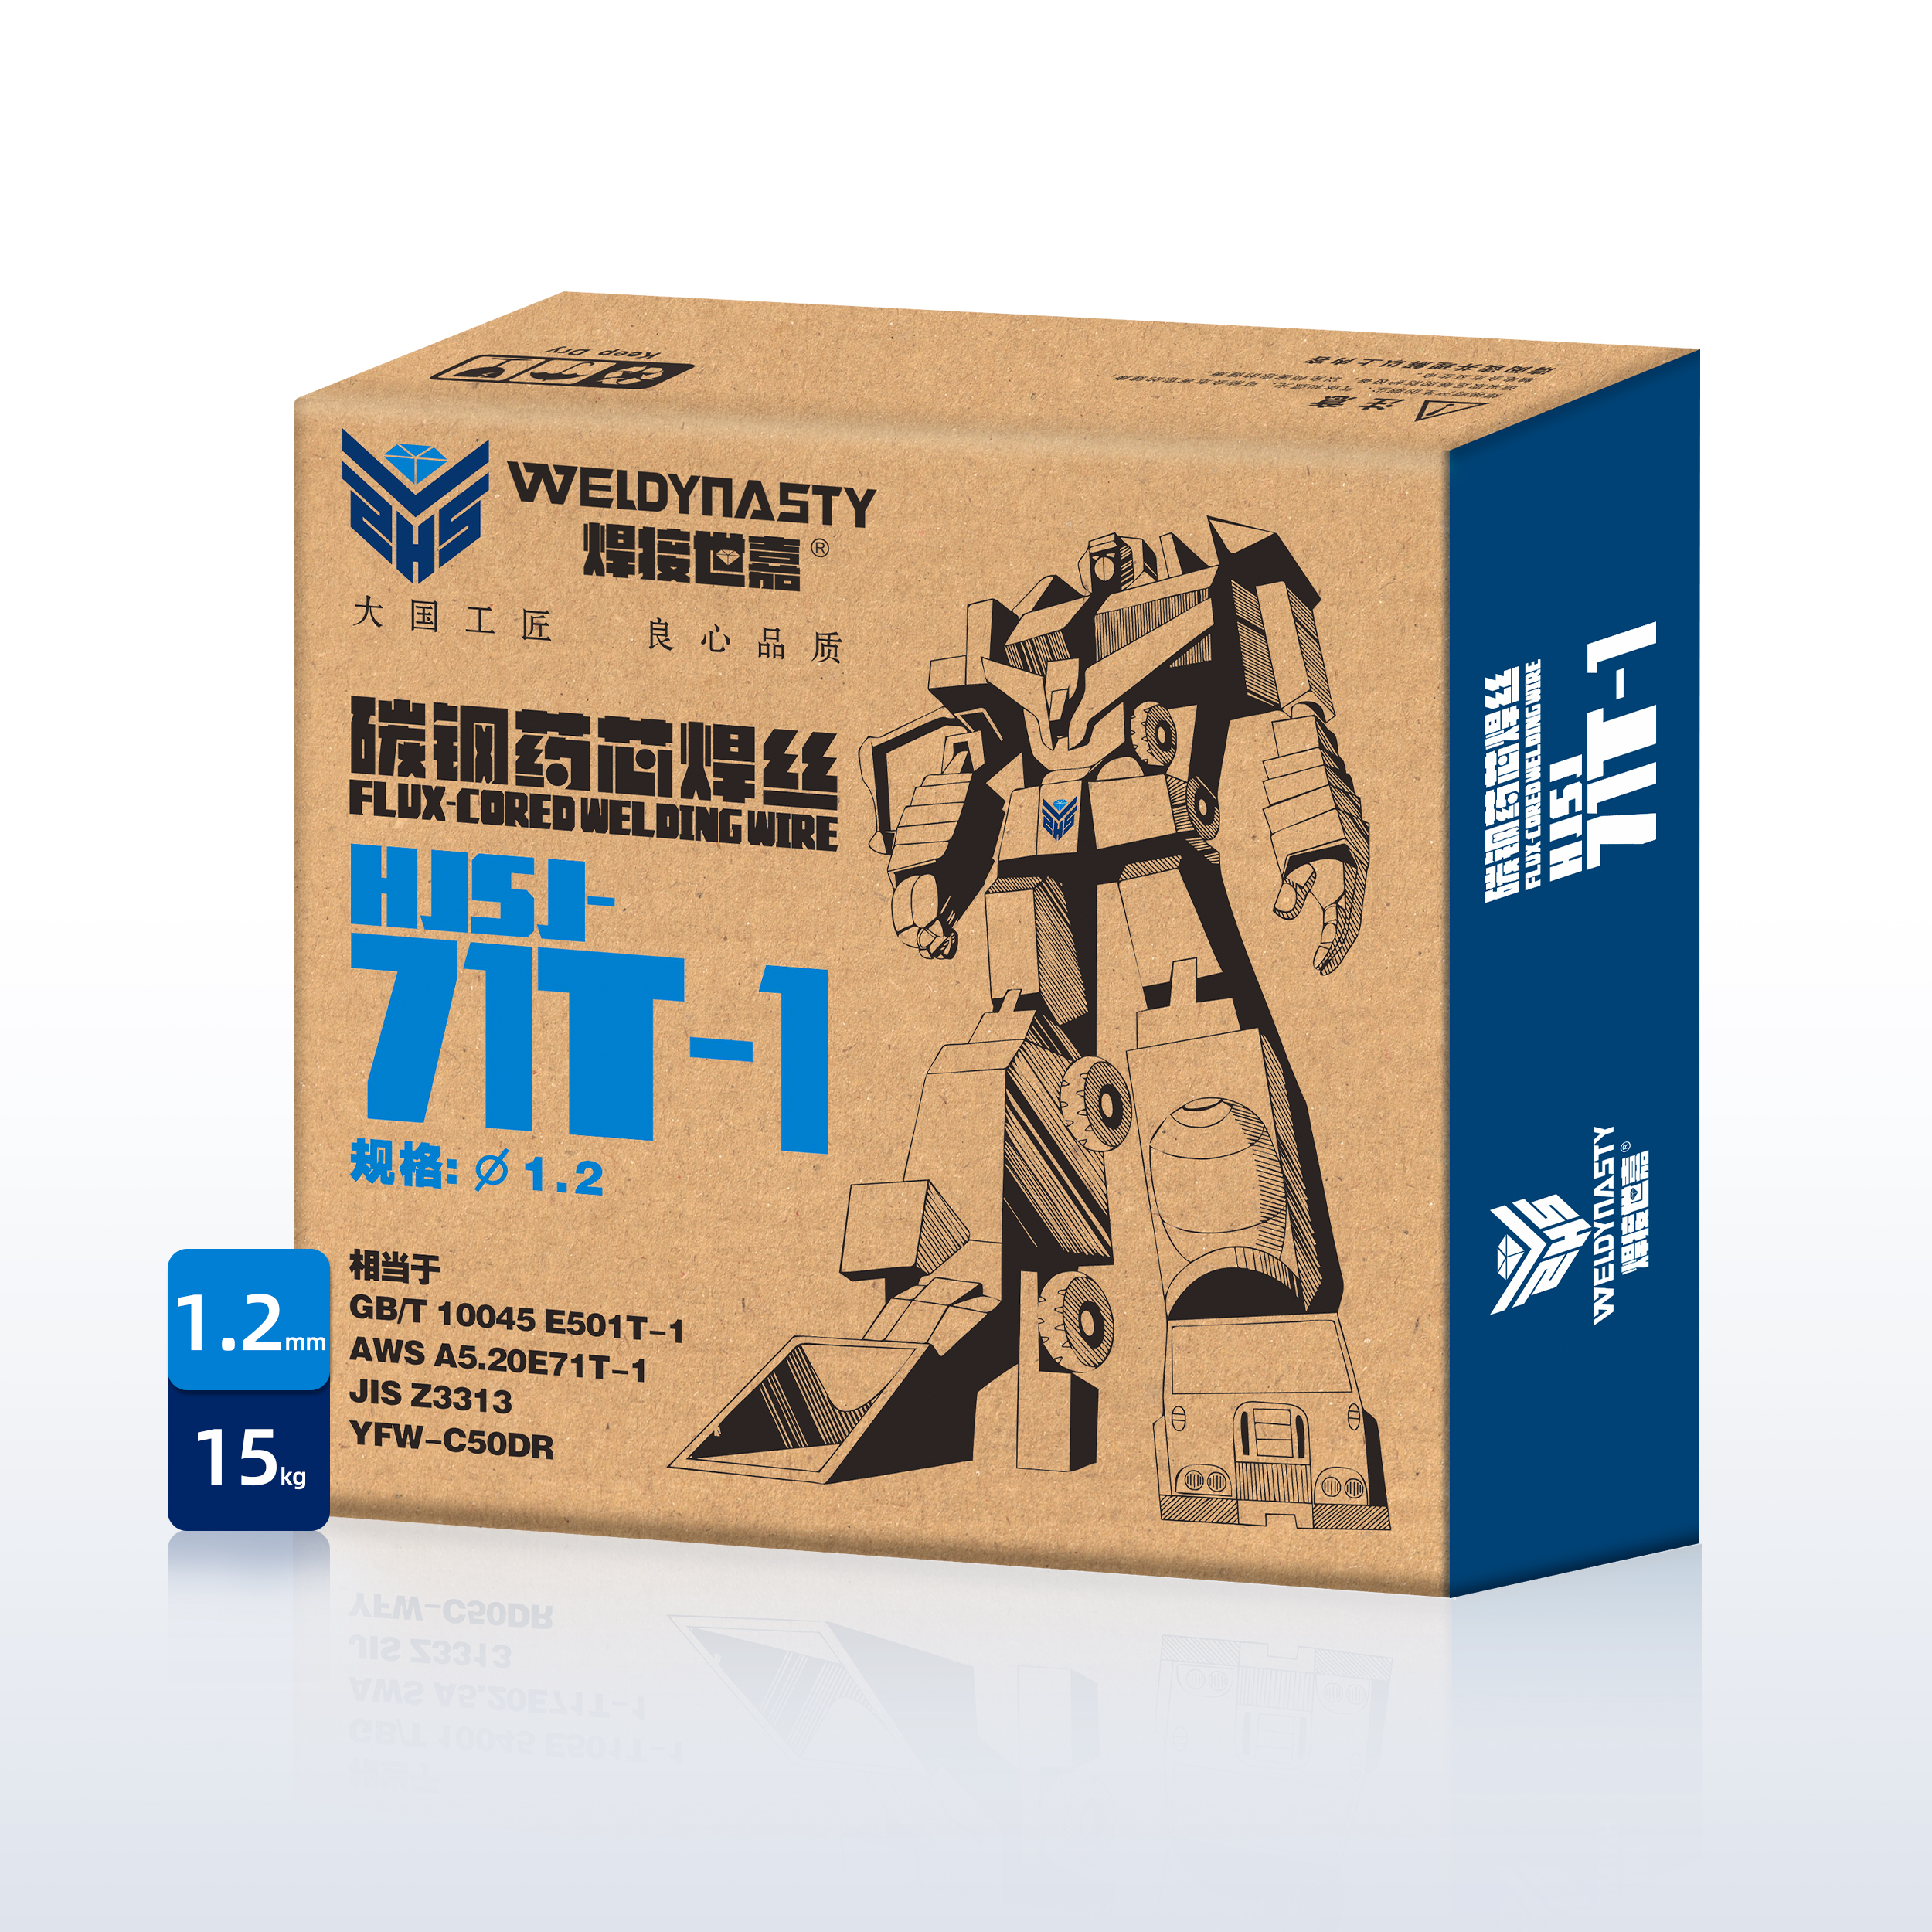
Available Diameters: Φ1.0, Φ1.2, Φ1.4, Φ1.6 mm
Welding Positions: Flat, horizontal, and all-position
Packaging: 15 kg/spool (standard); other packaging formats available (per requirement)
Shipbuilding, bridge construction, engineering machinery, marine engineering, coal mining machinery, and construction machinery
FAQ
Q1: What is the 71T-1 flux-cored wire designed for?
A: It is designed for demanding structural welding of carbon steel and low-alloy steel, combining a soft, stable arc with low spatter, easy slag removal, and micro-alloyed low-temperature toughness.
Q2: How does it compare with solid wire?
A: It offers a significantly higher deposition rate and improved current density, allowing faster wire melting and greater productivity than solid wire.
Q3: What polarity and shielding gas should I use?
A: Use DC+ (electrode positive) with 100% CO₂ shielding gas of purity ≥ 99.98%, at a flow rate of 20–25 L/min.
Q4: What welding positions are supported?
A: Flat, horizontal, and all-position welding, making it adaptable to both shop fabrication and field work.
Q5: What are the mechanical properties?
A: Tensile strength 490–670 MPa, yield strength ≥390 MPa, elongation ≥18%, and impact toughness ≥27 J at −20°C.
Q6: What are the classification standards?
A: AWS A5.20 E71T-1C (also GB/T 10045 T492T1-1C1A).
Q7: What diameters are available?
A: Φ1.0, Φ1.2, Φ1.4, and Φ1.6 mm.
Q8: How is it packaged?
A: Standard packaging is 15 kg/spool; other packaging formats are available per requirement.
Q9: What industries is it suitable for?
A: Shipbuilding, bridge construction, engineering machinery, marine engineering, coal mining machinery, and construction machinery.